High Care Food Facility Design Services
A high care food facility is a zone of a food manufacturing plant built specifically to protect ready-to-eat, allergen-sensitive or export-grade products from contamination, through strict segregation, airflow and hygiene design rather than general food factory standards. RMR Process designs, builds and helps certify high care facilities for Australian food manufacturers, whether that's a new high care zone or upgrading an existing brownfield site.
Understanding high care food processing requirements
High care applies wherever a product's risk profile demands more than standard food factory hygiene: ready-to-eat products, extended shelf-life foods, premium and allergen-sensitive lines, and export-oriented manufacturing where the customer or destination market sets its own compliance bar.
High care room design: the foundation of protection
High care room design starts with a risk assessment, then works through zoning strategy, traffic flow planning, air management design, surface specification and drainage and cleanability, in that order, so every later decision is built on an accurate picture of where contamination risk actually sits in the plant.
Key design elements for high care food processing
Airlock and anteroom systems, specialised flooring, wall and ceiling systems, and specialised LED lighting are the physical elements that make high care zoning actually work day to day, not just look compliant on paper.
High care construction standards: building for excellence
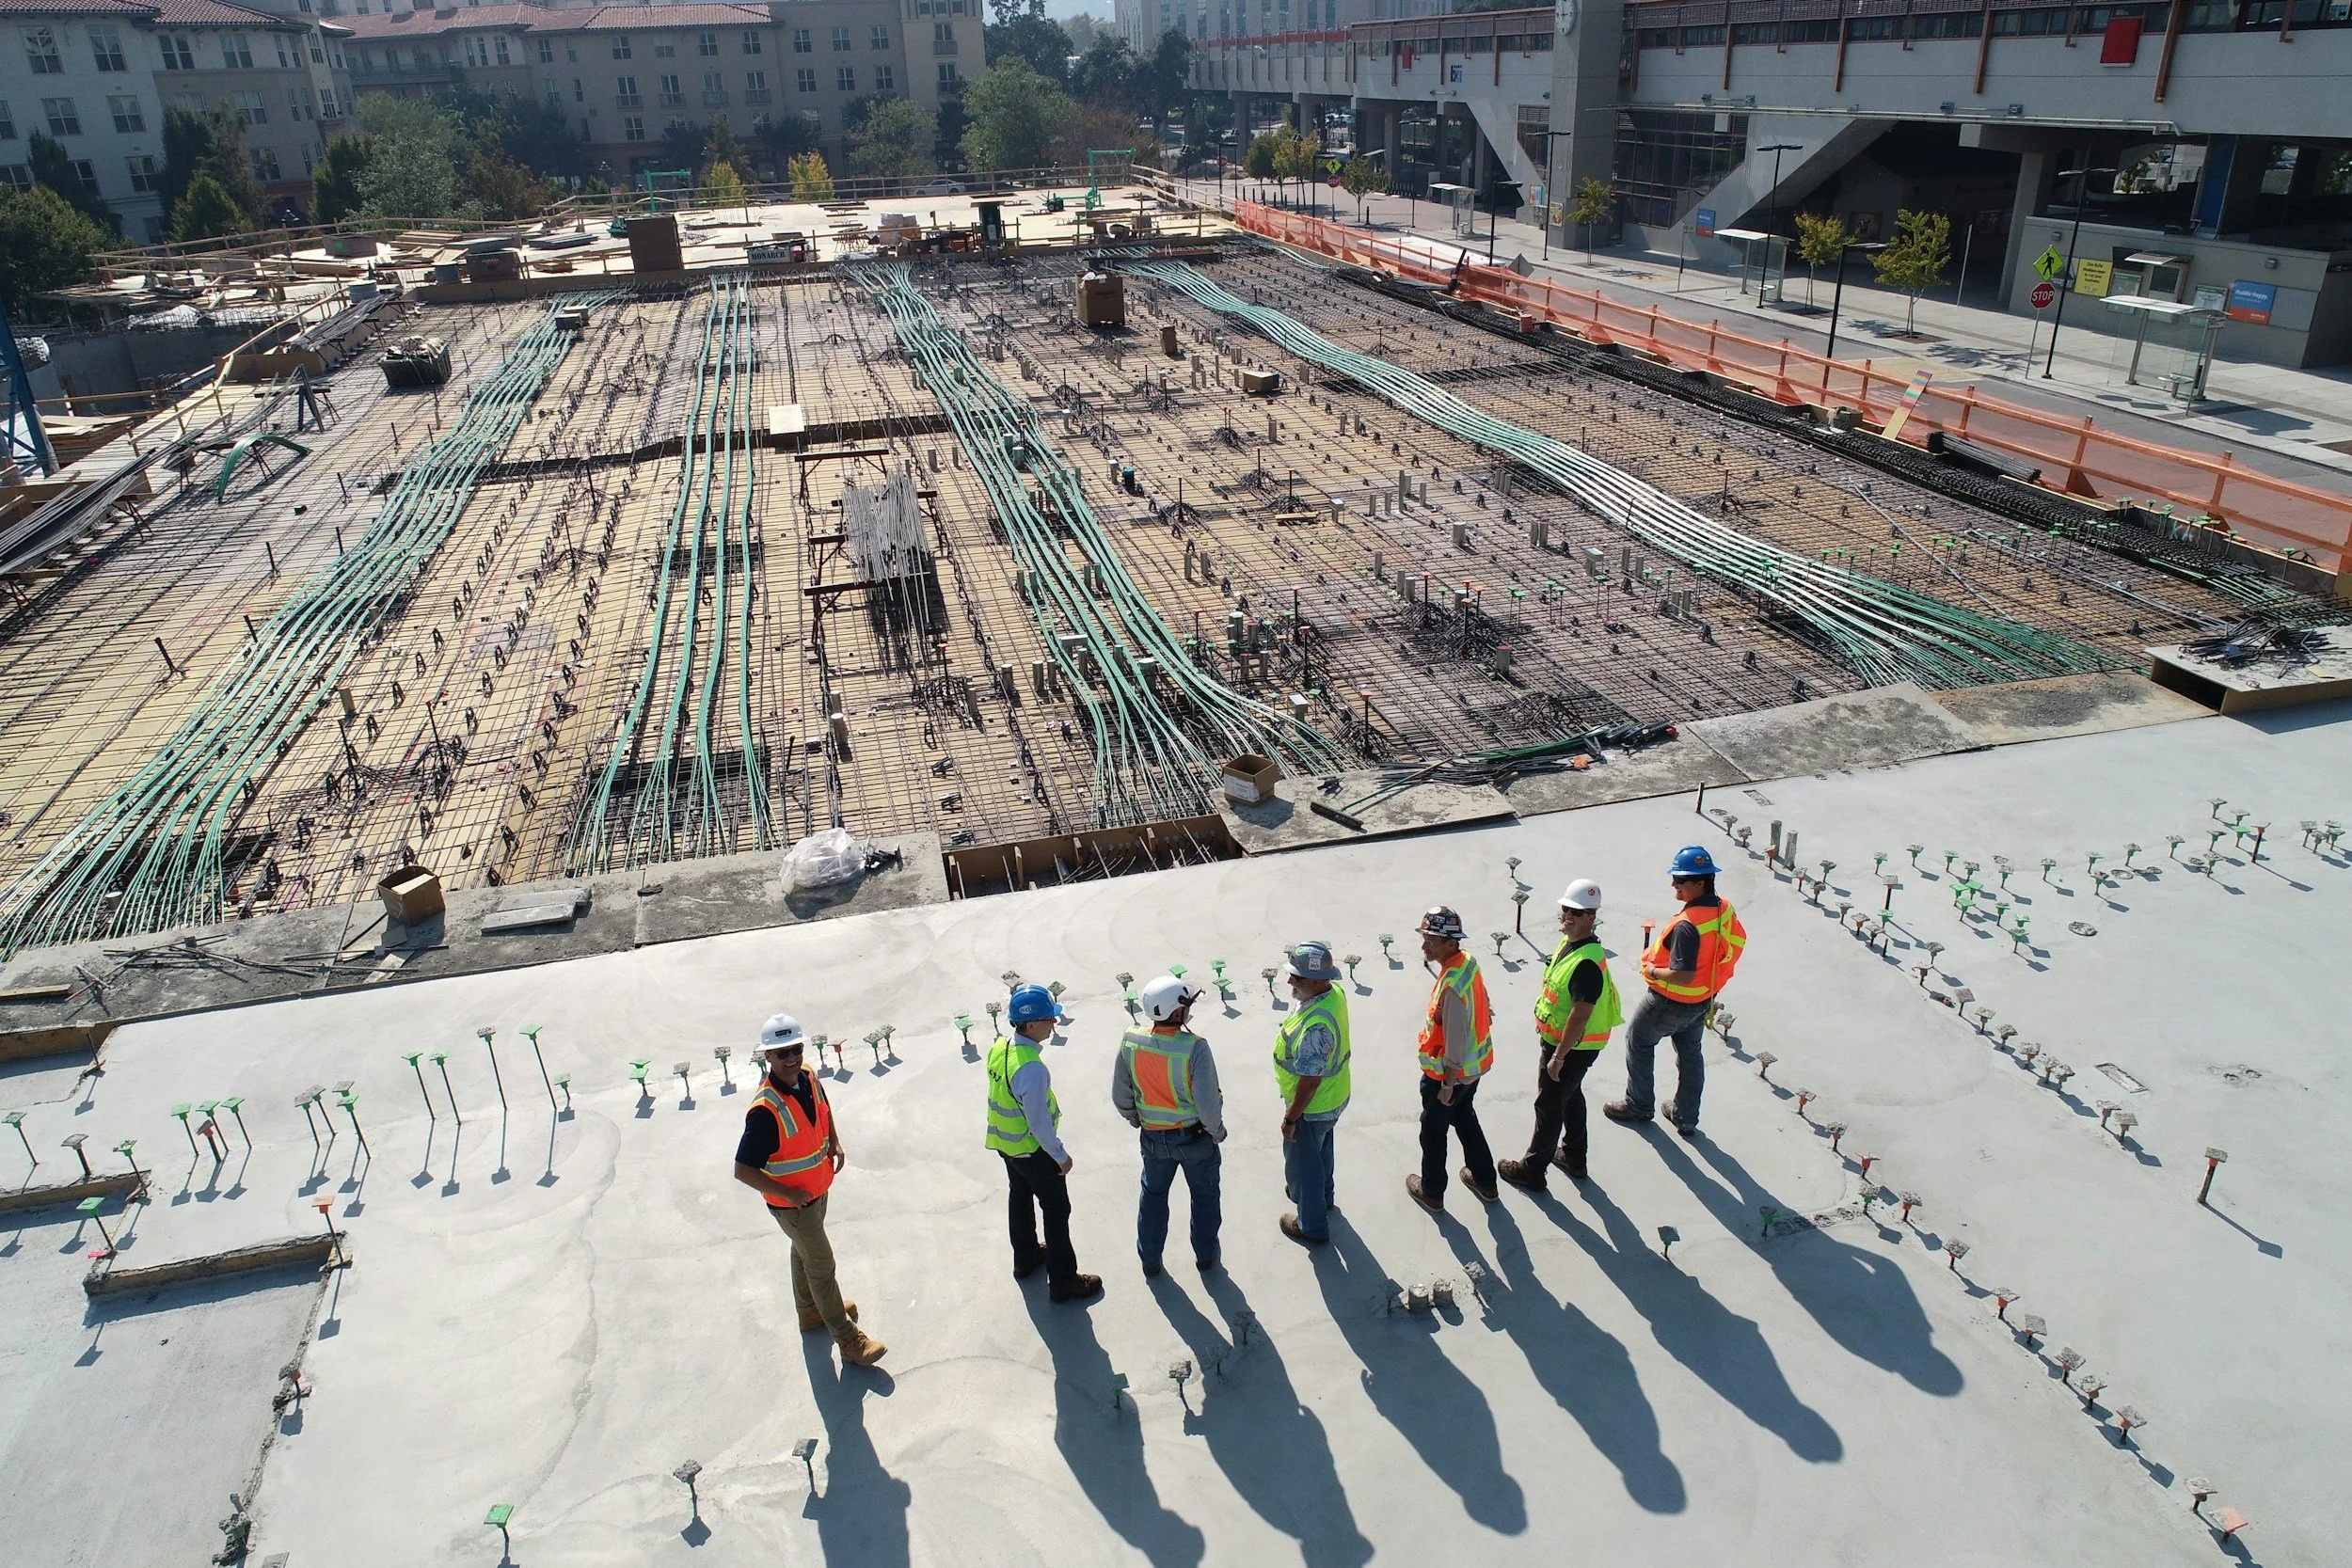
Construction quality is what determines whether a high care zone stays compliant under real operating conditions. RMR Process manages panel selection, joint treatment, service integration, door systems and window installation as one connected build, so hygiene performance doesn't degrade at the seams, service penetrations or doorways.
Case study: High Care Retrofit
An international specialty ingredients supplier needed to upgrade a brownfield facility to high care standards to meet its customers' requirements. RMR Process ran a full risk assessment, developed a zoning strategy and planned a phased implementation so the facility could keep operating through the works, then managed construction system selection and specialist contractors. The result was a fully compliant high care environment that achieved certification under customer audit, while minimising capital expenditure through the phased, strategically zoned approach.
Compliance
High care design at RMR Process is built around FSANZ requirements, HACCP integration, customer-specific standards, export market regulations and certification readiness, so compliance isn't a separate step bolted on at the end of the build.
High care technology integration
Air handling systems, automated cleaning systems, environmental monitoring tools and visualisation technologies can be integrated into a high care design to make ongoing compliance easier to maintain and demonstrate, not just achieve once at handover.
Ready to level up your manufacturing facility?
If your product range, customer base or export market now demands a high care standard your facility doesn't meet yet, talk to RMR Process about designing or upgrading that zone properly the first time. Contact us to discuss your high care facility requirements.
Modern high care food processing facilities benefit from specialised technologies that enhance protection while improving operational efficiency. Our technology integration services include:
Air Handling Systems - Specialised HVAC with appropriate filtration and monitoring
Automated Cleaning Systems - Integrated sanitation technologies for critical surfaces
Environmental Monitoring Tools - Real-time detection of environmental conditions
Visualisation Technologies - Remote monitoring capabilities for high care zones
These technologies enhance the effectiveness of high care environments while reducing operational burden and verification costs.
Partner with RMR Process for High Care Excellence
Whether you're implementing your first high care zone or upgrading existing facilities to meet new requirements, RMR Process provides the specialised expertise needed for successful high care food processing environments. Our integrated approach ensures that your high care facilities deliver appropriate protection while maintaining operational efficiency.
Contact us to discuss your high care facility requirements.


High Care Technology Integration
High Care Room Design
High Care Construction Standards
Regulatory Compliance
High Care Operations
High Care Technology Integration